Home › Products
Three product families, all built around the same core: bend the wire or tube, laser-cut the sheet-metal brackets, then weld it into one assembly the seat maker can bolt straight in. Everything we make is a wire-and-tube welded structure — see the scope note below for where that line runs on a front seat.
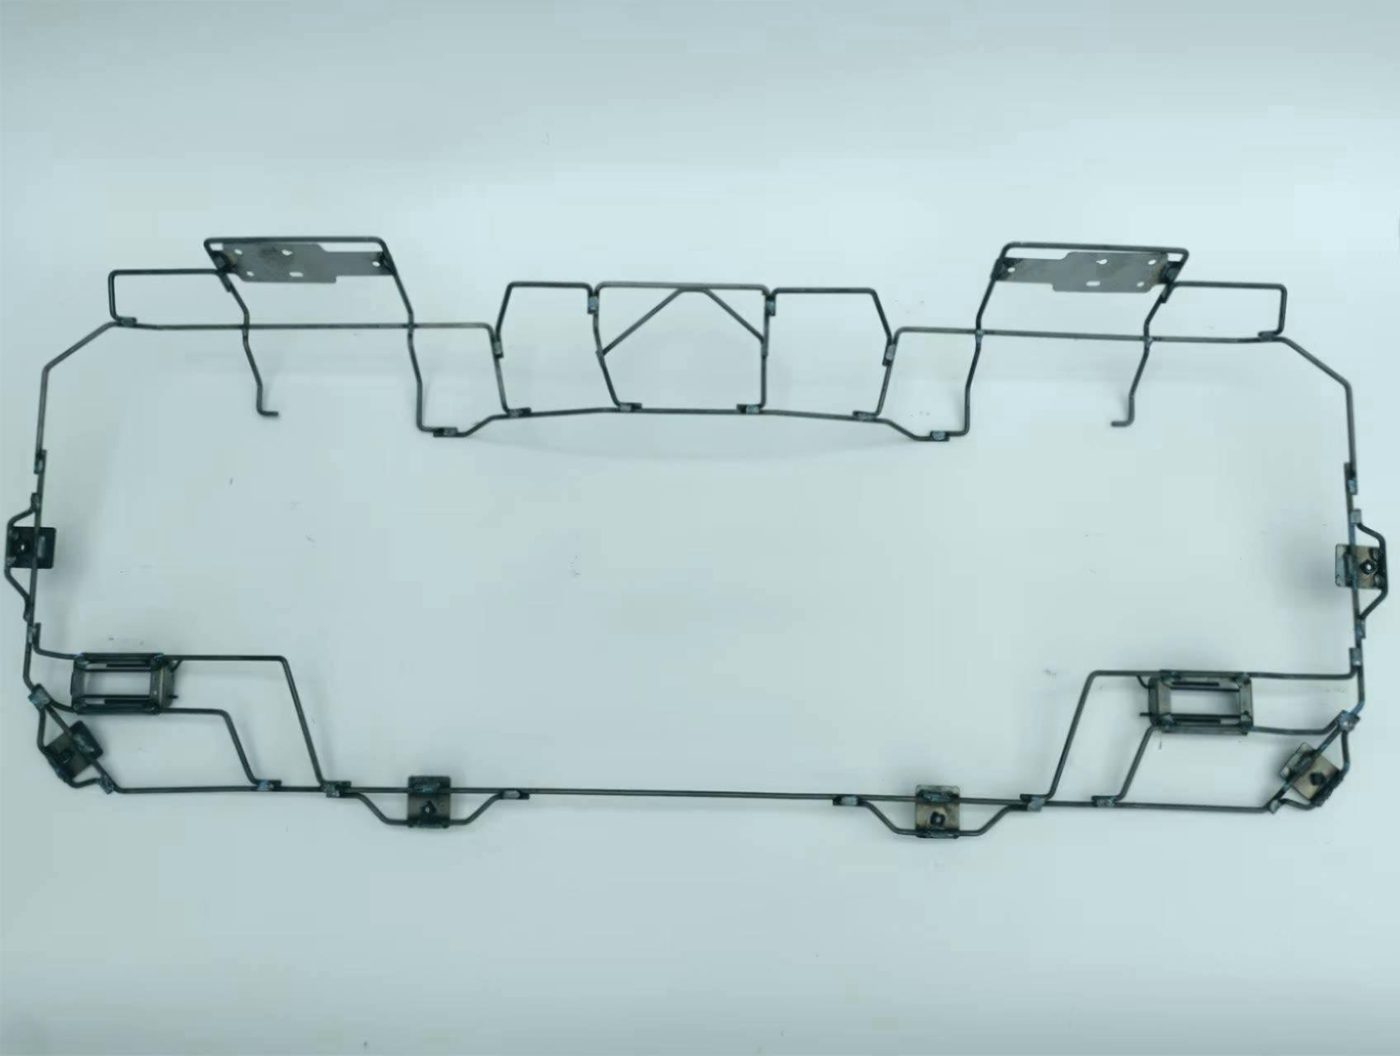
Our core product — the bent-wire frame that carries the cushion foam and the occupant on the rear bench. A typical assembly starts as coiled wire, bent to profile on a CNC wire bender, combined with laser-cut sheet-metal brackets, and then welded by robot into a single rigid structure.
Rear-seat structures are wire and tube structures, which is why a complete rear frame is ours to build. A front-seat structure is a different animal — predominantly stamped sheet-metal panels — and we do not build those. See the scope note at the end of this page.
We supply these to Tier-1 seat makers as a finished, inspected assembly ready for foam-over on the seat-maker's line. The finished part sits between the foam cushion and the seat pan and must meet the seat maker's dimensional, weld, and fatigue specifications.
We build to the seat maker's drawing and part number. We do not publish our customers' part numbers or programme names — yours will not appear here either.
Wire frames designed around EPP foam — expanded polypropylene, the light, impact-absorbing material used in seat backs and headrests that must meet energy-management targets.
The wire frame inside an EPP part performs two jobs: it carries the foam mechanically during assembly, and it provides the fixing points to the seat structure. We form the wire profile to the mould geometry, weld in any required inserts or clips, and deliver the bare frame to the foam moulder.
Supplied LH/RH as the programme requires.
Not every programme needs a complete cushion assembly. We also supply the individual sub-components that go into a seat structure — either on their own or welded into the cushion assembly above.
These parts are quoted on the same three-line basis as a full assembly: part processing cost, tooling amortisation, and outsourced surface treatment each as a separate line.
We make: wire and tube welded structures. Complete rear-seat cushion and back frames; cushion support tubes, suspension wires, adjuster links and brackets for any seat, front or rear; EPP wire frames.
We do not make: the front-seat frame itself. A front-seat structure is predominantly stamped sheet-metal panels, and large sheet-metal stamping is not a process we run. On a front seat we supply the wire and tube parts that mount on that structure — not the structure.
Not sure which side of that line your part falls on? Send the drawing. We will tell you within 3 working days, before either of us spends time on a quotation.
Everything from raw wire and tube to a welded, inspected assembly happens on our floor. Surface treatment (e-coat, zinc plating) is the one step we place with qualified outside processors — and we say so up front rather than implying we plate in-house.
Installed capacity against what we actually ran in 2025. The gap is the room a new programme can move into without displacing an existing one.
Production runs in a 9,000 m² plant with 8,200 m² of production floor in Hannan District, Wuhan — our third move since the company was founded in September 2001, completed in 2025 — with a further 3,000 m² production base in Guangzhou.